Get 30% OFF on Maharani Products

Infrastructure

Automated milling, large-scale warehousing and export-ready logistics behind every grain of Maharani Basmati Rice.

Infrastructure That Powers Global Excellence

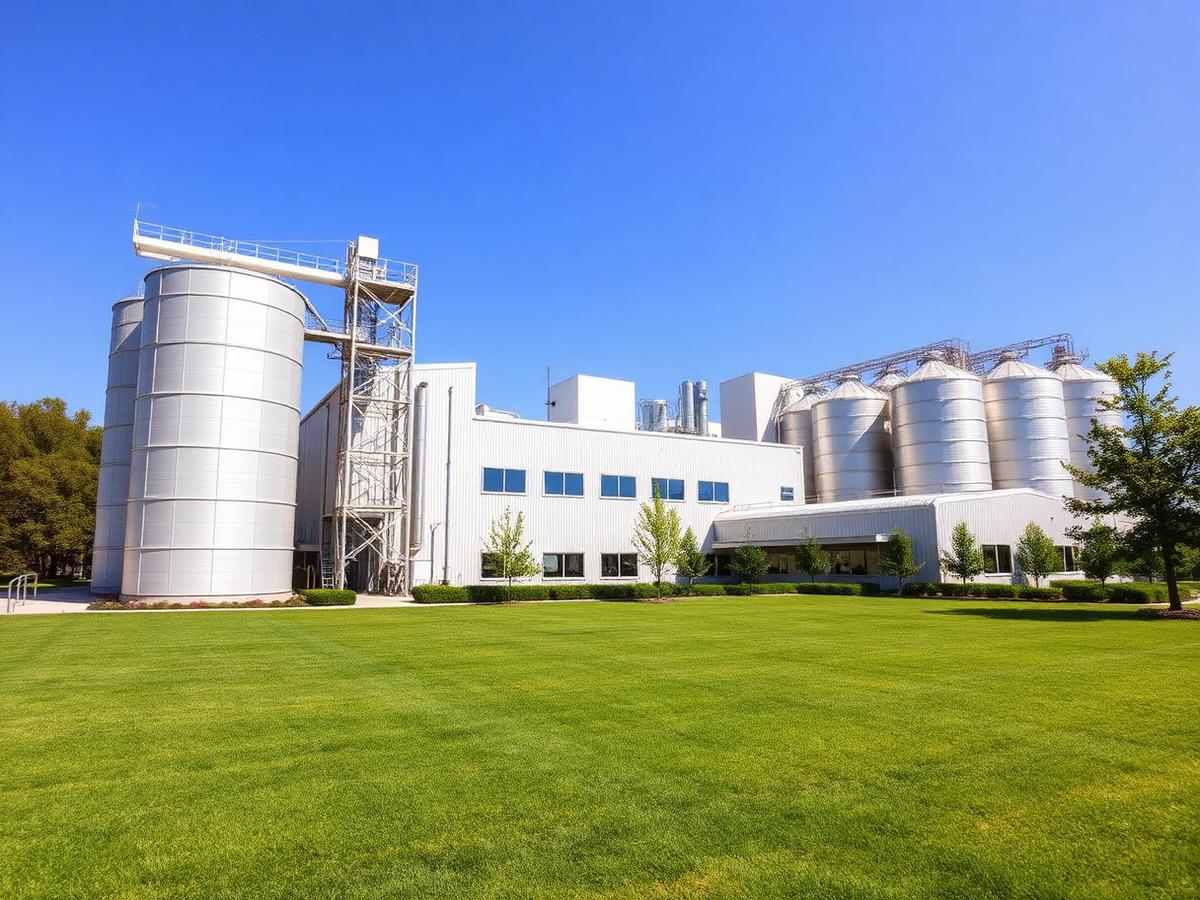
At Chaman Lal Setia Exports Ltd., our world-class infrastructure stands as a symbol of precision and scale. With three fully automated rice milling plants built with the latest technology, we ensure flawless paddy processing and uniform grain quality at every stage. Our integrated paddy-to-rice production capacity exceeds 750 metric tonnes per day, while our rice packing lines operate at over 1,000 MT per day — enabling us to meet global demand efficiently.
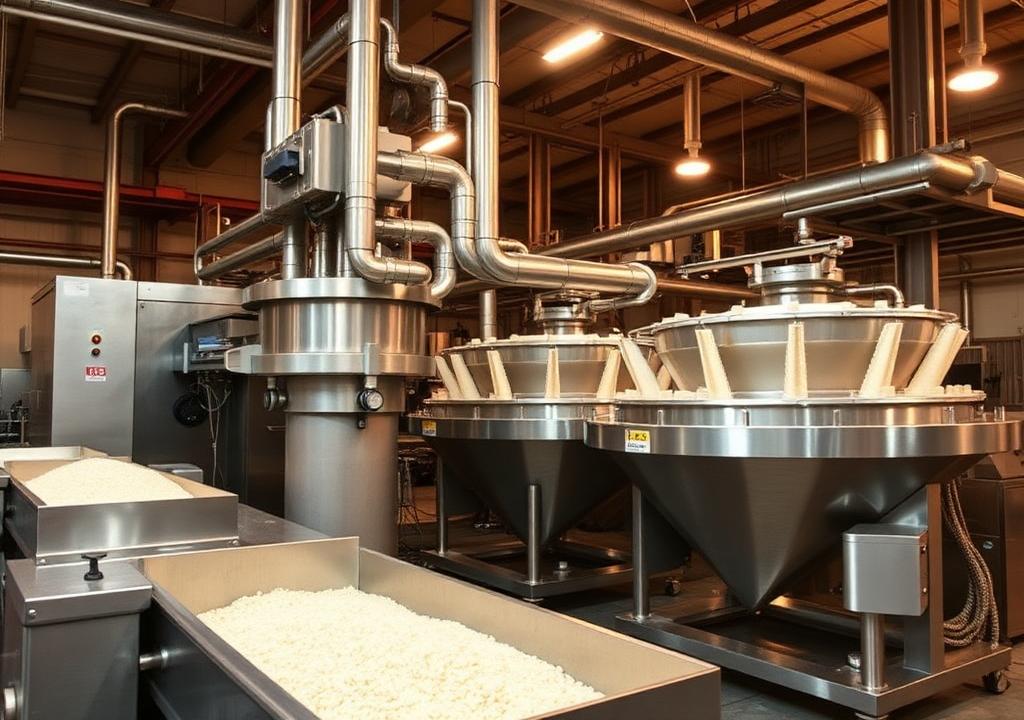
Automated rice milling machinery inside the Maharani processing plant

Unmatched Global Warehousing

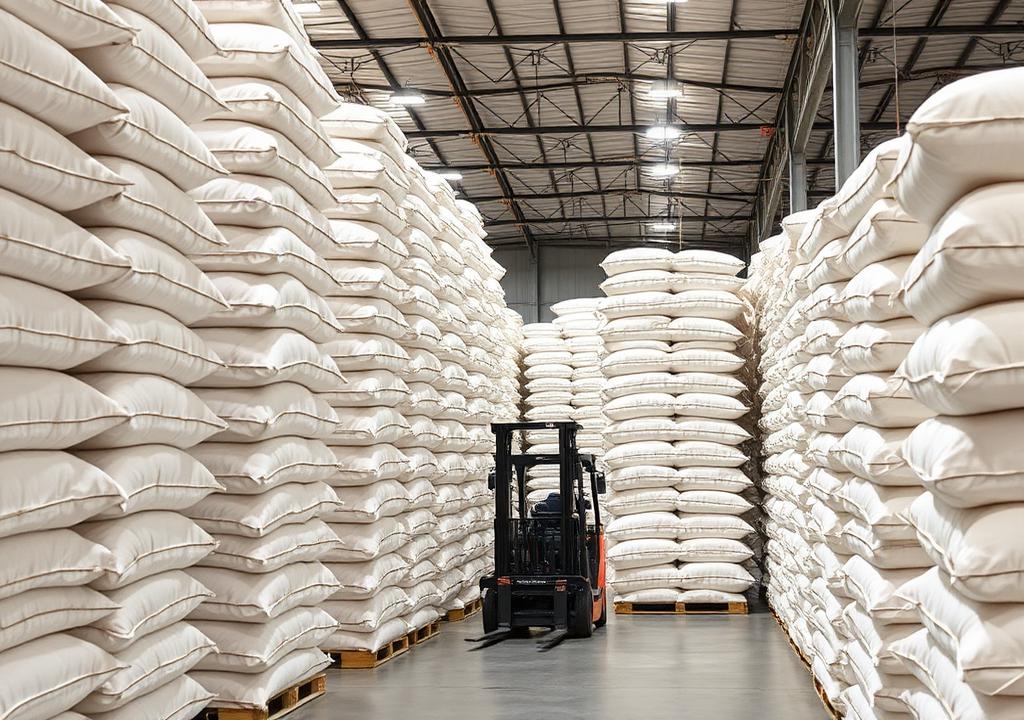
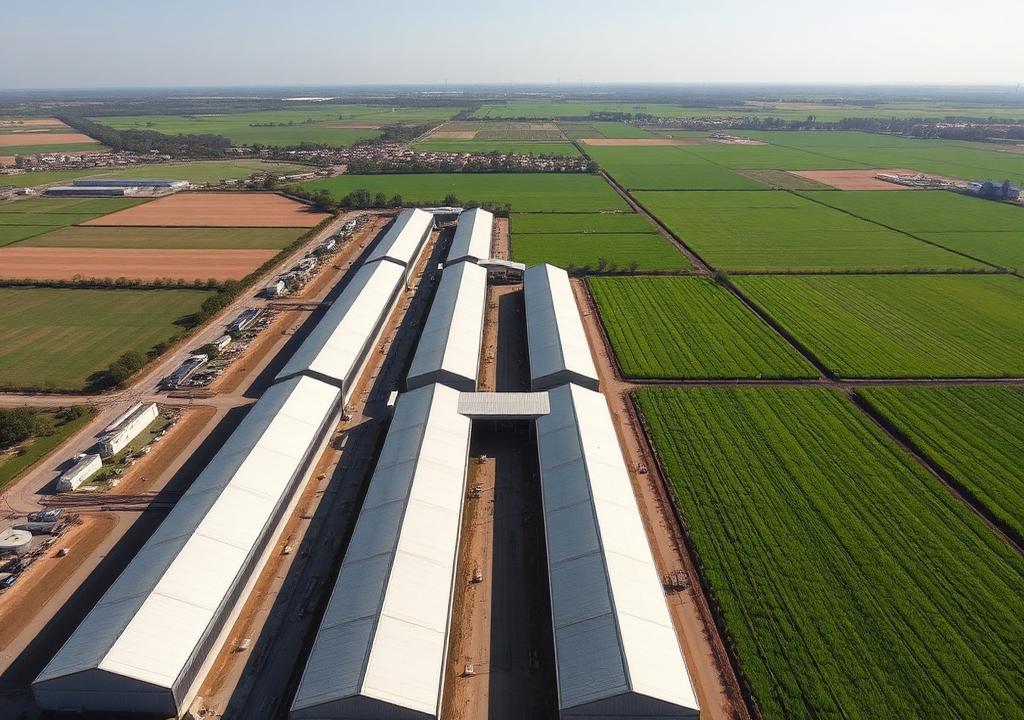
Spanning over 1 million square feet, our advanced warehousing network ensures that every grain is stored under ideal conditions. Each facility is temperature-regulated, hygienically maintained and supported by a digital inventory management system for real-time monitoring. From bulk stockpiling to export packaging, our warehousing system enables seamless logistics and timely shipments to international destinations.

Aerial view of the Maharani warehousing complex

Quality at Every Step

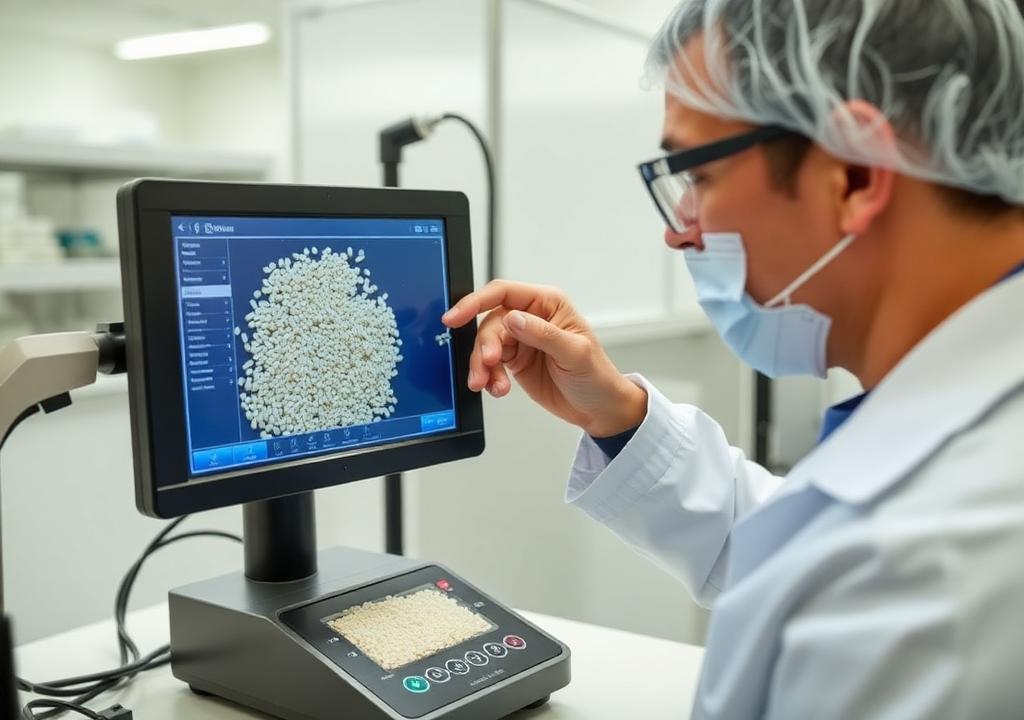
Our commitment to quality is uncompromising. Certified with 13 international quality standards, we follow rigorous inspection and testing protocols at every phase — right from raw paddy selection to final export-ready packaging. Advanced laboratories, skilled technicians and strict adherence to food-safety norms ensure that every sack of rice meets the highest benchmarks of purity, taste and consistency.

Laboratory technician inspecting basmati rice grains

Global Reach & Reliability

With exports to 95+ countries, 600+ private label brands and 35+ containers dispatched daily, our infrastructure reflects the strength of a company built on legacy and innovation. Backed by over 50 years of excellence, Chaman Lal Setia continues to redefine global standards in rice milling, packaging and export logistics.

Stacked rice sacks ready for export in a Maharani warehouse

Facilities & Capabilities

Every unit is designed to keep quality consistent from paddy intake to final container dispatch.

3 Automated Mills

Fully automated paddy-to-rice lines with modern colour sorting.

750+ MT / Day

Integrated milling capacity to serve large export programmes.

1 Mn Sq Ft Storage

Temperature-regulated, hygienically maintained warehousing.

13 Certifications

International quality and food-safety standards across units.

1,000 MT Packing

High-speed packing lines for retail, bulk and private label.

35+ Containers Daily

Export logistics reaching 95+ countries around the world.

Our Process

Four controlled stages that carry each grain from the field to the export container.

01

Paddy Sourcing

Selected from trusted growing belts and graded on arrival.

02

Ageing & Milling

Naturally aged, then milled on automated precision lines.

03

Sorting & Testing

Colour sorting and laboratory checks for purity and length.

04

Packing & Export

Hygienic packing, container loading and documented dispatch.

50+

Years of Legacy

95+

Countries Served

600+

Private Label Brands

1 Mn

Sq Ft Warehousing

Gallery

A closer look at our mills, warehouses, laboratories and export operations.

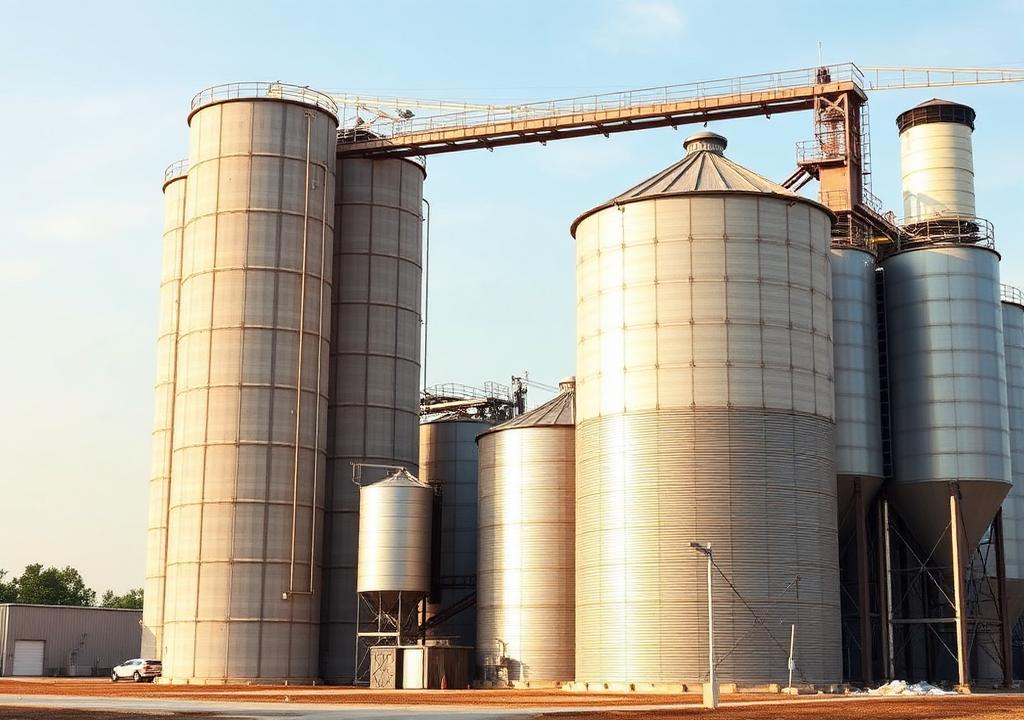
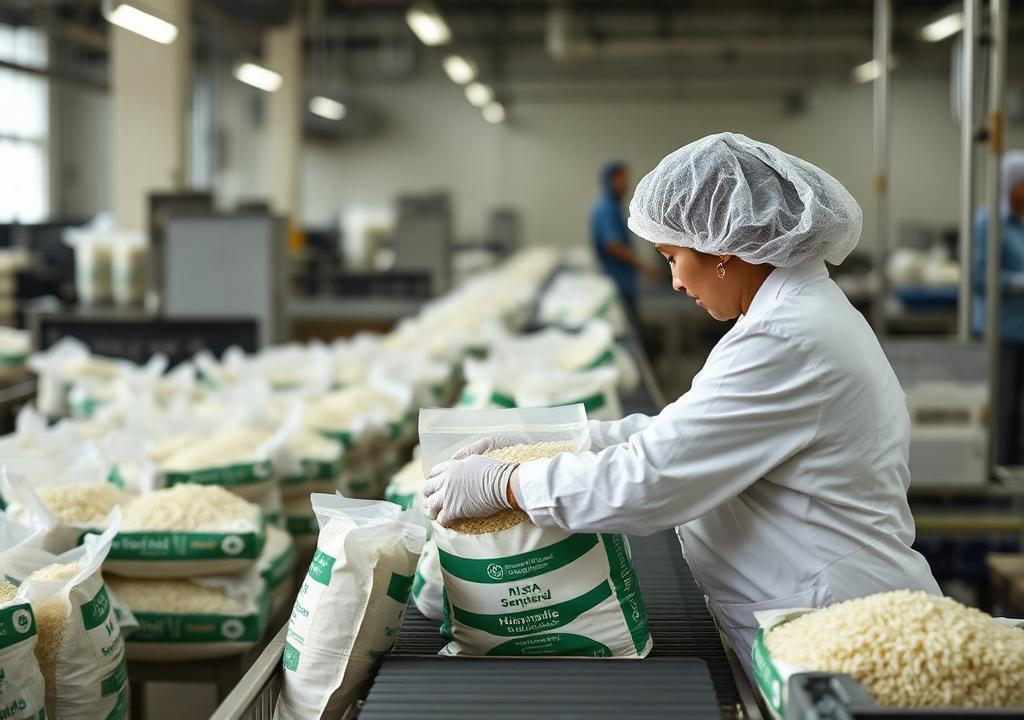
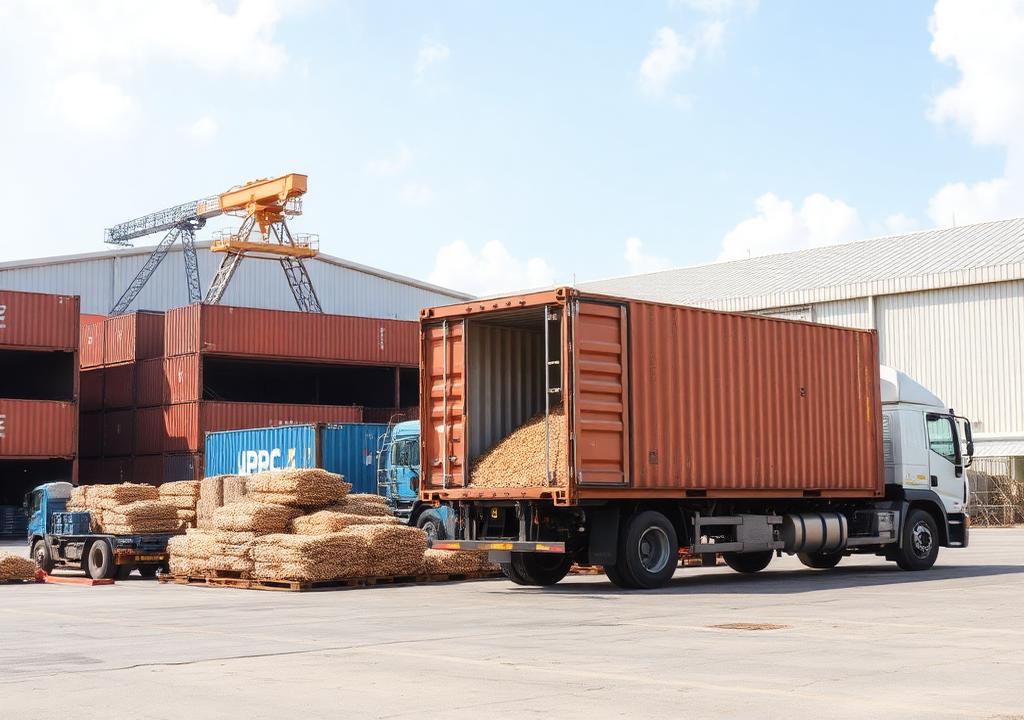
Grain storage silos at the rice processing plant Maharani rice processing facility exterior Rice bags being packed on the production line Container truck loading at the export yard Automated milling equipment in operation Quality laboratory testing of rice grains Aerial view of the warehousing complex Rice sacks stacked in the storage warehouse Maharani basmati rice presentation

Planning a bulk or private label order?

Our export desk will walk you through capacity, certifications and shipping timelines.

Talk To Our Team